
High-performance MVE Vibrator Motor: An In - depth Exploration
MVE vibrator motors are a crucial component in various industrial applications. They come in differe
High-performance MVE Vibrator Motor: An In - depth Exploration
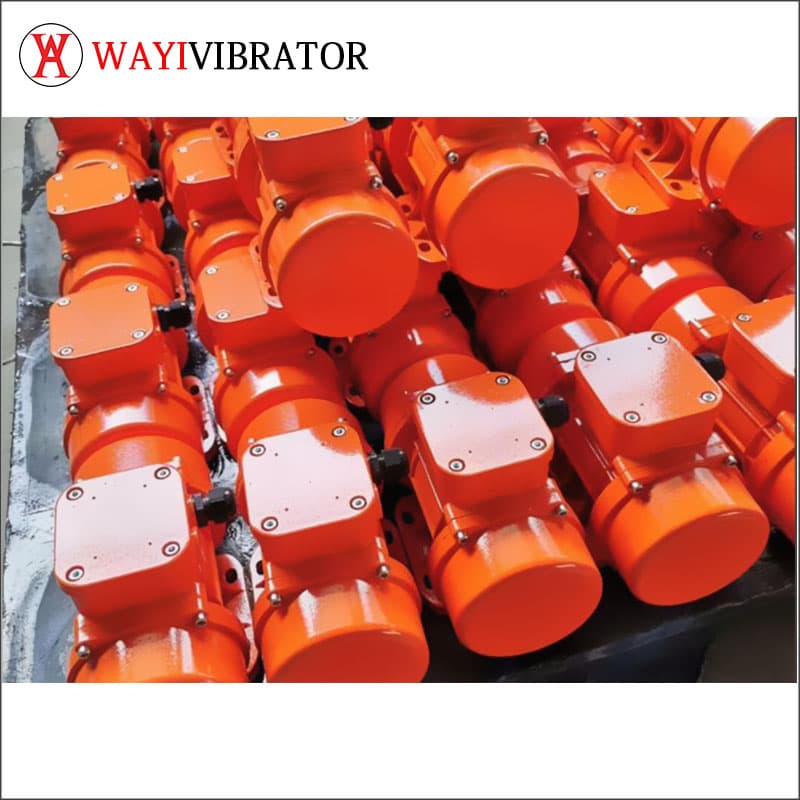
Introduction to MVE Vibrator Motors
MVE vibrator motors are a crucial component in various industrial applications. They come in different models, such as the MVE200/3N - BLDC - 23A0 - 24V from WAYIVIBRATOR, and a range of other MVE series motors like MVE800/3M, P60, and MVE10000/1. These motors are designed to provide reliable and efficient vibration for different industrial processes.
The MVE series standard vibration motors have a wide range of adjustable excitation forces, from 20 - 40000 kg. This wide range allows them to meet the requirements of various industrial vibration equipment. They are available in three - phase, single - phase, and DC motor types, which gives users more choices according to their specific needs.
Technical Features of MVE Vibrator Motors
Sturdy Design
MVE horizontal vibration motors feature a robust cast - iron base designed using finite element analysis. This design ensures the motor's durability and stability, even in harsh industrial environments. The use of advanced design techniques helps the motor withstand mechanical stress and vibration over an extended period.
Eccentric Block Mechanism
Inside the motor, there is a motor unit, and at both ends of the shaft, there are eccentric blocks. When the vibration motor is turned on, the high - speed rotation of these eccentric blocks generates centrifugal force. This centrifugal force is the source of the vibration that the motor produces. The design of the eccentric blocks can be adjusted to control the amplitude and frequency of the vibration, which is crucial for different applications.
Certification and Safety
MVE vibrator motors have ATEX ExII3D and ETL, Class II, Division 2 certifications. These certifications indicate that the motors can be used in environments where there may be combustible dust. This safety feature makes them suitable for a wide range of industrial settings, including those with potential fire or explosion hazards.
Performance Metrics of MVE Vibrator Motors
Excitation Force
As mentioned earlier, the excitation force of MVE series motors can be adjusted from 20 - 40000 kg. For example, the MVE200/3N - BLDC - 23A0 - 24V has an excitation force of 198 kg. This force is essential for driving the vibration equipment to perform tasks such as material conveying, screening, and compaction. Different applications require different levels of excitation force, and the wide range of the MVE series allows for precise matching.
Vibration Frequency
The vibration frequency of MVE motors is also an important performance metric. Some motors, like the one with a rated speed of 8800 RPM, can generate high - frequency vibrations. The frequency of vibration affects the efficiency and effectiveness of the industrial process. For example, in material screening, a higher frequency may be more suitable for separating fine particles.
Power and Current Consumption
The power and current consumption of MVE vibrator motors are designed to be efficient. The MVE200/3N - BLDC - 23A0 - 24V has an excitation power of 0.16 KW and a current of 6.7A. This relatively low power consumption helps reduce energy costs in industrial operations while still providing sufficient vibration power.
Applications of MVE Vibrator Motors
Material Handling and Conveying
MVE vibrator motors are widely used in material handling systems. They can be installed on conveyors to help move materials more smoothly. By generating vibrations, the motors can prevent materials from sticking to the conveyor surface and ensure a continuous flow of materials. For example, in a mining operation, MVE motors can be used to convey ores from one processing stage to another.
Screening and Classification
In industries such as agriculture, mining, and recycling, MVE motors are used for screening and classification. The vibrations generated by the motors help separate materials of different sizes. For instance, in a grain processing plant, MVE motors can be installed on a screening machine to separate different grades of grains.
Compaction and Densification
MVE motors can also be used for compaction and densification applications. In the construction industry, they can be used to compact soil or concrete. By applying vibrations, the motors help reduce the voids in the material, increasing its density and strength.
Material Discharge from Silos and Hoppers
When installed on silos or hoppers, MVE vibrator motors can assist in material discharge. They can break up bridges and arches formed by materials inside the silo or hopper, ensuring a smooth and continuous flow of materials. This is particularly useful in industries such as food processing and chemical manufacturing.
Comparison with Other Vibrator Motors
Advantages over Traditional Motors
Compared with traditional vibrator motors, MVE motors have several advantages. Their wide range of adjustable excitation forces allows for more flexibility in different applications. The advanced design of the eccentric block mechanism provides more precise control over vibration parameters. Additionally, the certifications they hold make them safer to use in hazardous environments.
Performance in Different Environments
In harsh industrial environments, MVE motors perform better than some other motors. Their sturdy cast - iron base and high - quality components make them more resistant to wear and tear. In environments with combustible dust, the safety certifications of MVE motors give them an edge over non - certified motors.
Cost - effectiveness
Although the initial cost of MVE motors may be higher than some basic vibrator motors, their long - term cost - effectiveness is significant. Their energy - efficient design reduces power consumption, and their durability means less frequent replacement and maintenance, resulting in overall cost savings for industrial users.
Future Developments and Trends of MVE Vibrator Motors
Technological Innovations
In the future, we can expect to see more technological innovations in MVE vibrator motors. This may include the use of more advanced materials in the motor construction to further improve durability and reduce weight. The development of intelligent control systems may also allow for more precise adjustment of vibration parameters based on real - time feedback.
Expansion of Application Areas
As industries continue to evolve, the application areas of MVE vibrator motors are likely to expand. For example, in the emerging field of advanced manufacturing, MVE motors may be used in new types of production equipment. In the environmental protection industry, they may be used in waste treatment and recycling processes.
Market Competition and Growth
The market for MVE vibrator motors is expected to face increasing competition. However, with their high - performance features and continuous innovation, MVE motors are well - positioned for growth. Manufacturers may need to focus on improving product quality, reducing costs, and providing better customer service to stay competitive in the market.
In conclusion, high - performance MVE vibrator motors play a vital role in modern industrial applications. Their technical features, performance metrics, and wide range of applications make them a popular choice for various industries. As technology advances and market demands change, MVE vibrator motors are likely to continue to evolve and contribute to the development of the industrial sector.


More than 500 partners,
More than 200 models,
Best choice of high quality and good price from China
Provide suitable, high-quality, and multiple vibrators to support your work. Cooperation is the best way to success


